Inquiring about coloration
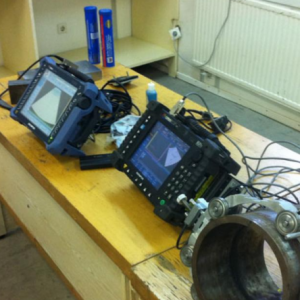
Subject: Technical Support Request – PAUT and TOFD Calibration, Group Configuration, and Scan Plan for ADNOC Vessels and Towers
Dear Technical Support Team,
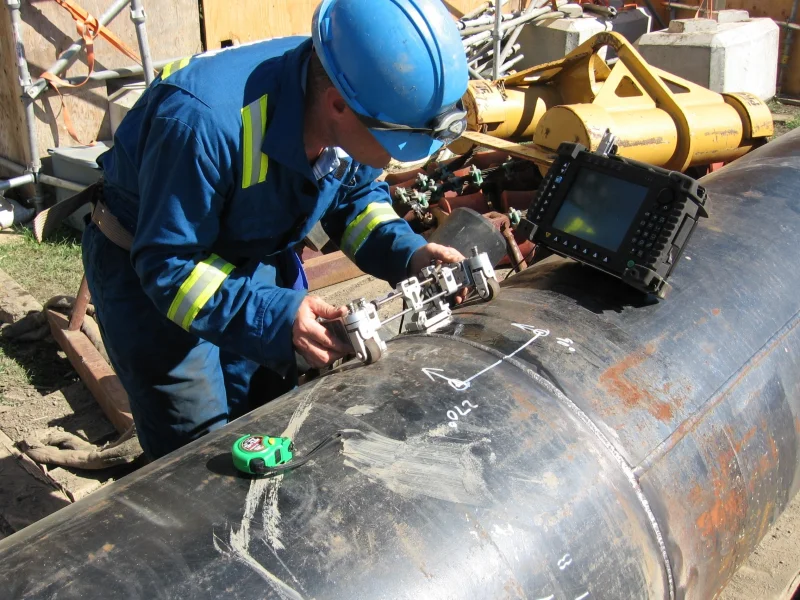
We are currently working on a project for ADNOC involving the inspection of vessels and towers with the following material thicknesses:
- 18 mm
- 72 mm
- 82 mm
- 110 mm
- 140 mm
Only the 110 mm thickness specimen has a 3 mm cladding layer (110 mm + 3 mm clad). The remaining thicknesses are unclad.
We are required to perform PAUT and TOFD calibration for each of these thicknesses. We have already obtained demonstration calibration blocks with the same P-Numbers and corresponding thicknesses as the components being inspected. These blocks contain Side-Drilled Holes (SDHs) positioned at 1/4T, 1/2T, and 3/4T.
We would appreciate your technical guidance on the following points.
1. PAUT and TOFD Calibration
- What is the recommended calibration procedure for each thickness, for both PAUT and TOFD?
- How many PAUT groups or focal-law groups should be used for each thickness, and what is the technical justification for selecting that number?
- Which probe types, frequencies, element configurations, and wedges would you recommend for each thickness?
- Are SDHs at 1/4T, 1/2T, and 3/4T sufficient for calibration, or are additional reflectors or calibration steps required?
2. PAUT Setup for the 82 mm Thickness
We are currently inspecting the 82 mm thickness using two PAUT groups, with the following probe and wedge configuration:
- Probe: A32-5L-32
- Wedge: SA3-55S-IHC
We would like to confirm whether this configuration is suitable and whether two groups are sufficient to achieve adequate weld-volume coverage.
Specifically, we would appreciate your recommendations regarding:
- Preferred beam angle range, including the start and stop angles.
- Recommended scanning technique.
- Suitable probe and wedge configurations.
- Appropriate focal-law and focal-depth settings.
3. Scan Plan Direction Versus Actual Scanning Direction
We have another important technical question regarding TOFD inspection.
Suppose we create the scan plan based on scanning from the outside of the vessel, including the complete weld bevel geometry and assuming that the probe will be positioned on the external surface.
However, during the actual inspection, we perform the TOFD scan from the inside of the vessel, along the internal surface of the circumferential weld (CWL).
Would this difference between the scan-plan orientation and the actual scanning surface affect the inspection results, sound paths, lateral-wave and back-wall positions, defect depth and height measurements, or the reliability of defect characterization?
Is it acceptable to use a scan plan created for external scanning when the actual scan is performed internally, or must the scan plan be modified to represent the actual scanning surface and weld geometry?
4. Selecting the Number of PAUT Groups
We would also appreciate a detailed explanation of when to use a single PAUT group and when multiple groups are required.
- What factors determine the appropriate number of groups for each material thickness?
- How do weld preparation geometry, bevel angle, root configuration, probe aperture, refracted beam angles, and required weld-volume coverage influence this decision?
- How should we determine the appropriate angle range and focal-law configuration for each thickness?
- How should we select the focal depth and focal-law settings to ensure adequate coverage of the weld root, fusion faces, weld body, and upper and lower regions?
Our objective is to establish a technically sound and code-compliant PAUT and TOFD inspection procedure for all five thicknesses, including the 110 mm + 3 mm clad configuration.
We would appreciate your recommendations, including any applicable technical documentation, calibration procedures, or recommended setup parameters.
Thank you for your support.
Best regards,
PAUT/TOFD Inspection Team
0 replies
Sign in to reply to this discussion.