Join free
 Register your company
 Sign in
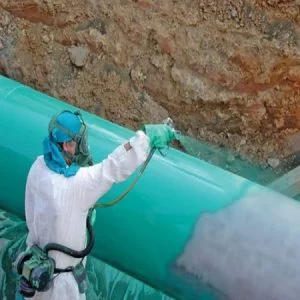
Welcome to NDT Inspect's coating and paint inspection group, a place for professionals to connect and discuss the latest techniques and technologies in the inspection of coatings and paints.
Coating and paint inspection is a critical aspect of ensuring the quality and durability of coated and painted surfaces, and it is used in a variety of industries, including automotive, construction, and manufacturing.
Coating and paint inspection can involve a range of methods and techniques, including visual inspection, thickness measurement, adhesion testing, and corrosion testing. These methods are used to evaluate the condition and performance of coatings and paints on various surfaces, including metal, concrete, and wood. Our member group offers a platform for sharing knowledge and best practices on coating and paint inspection and its applications in various industries.
Join our community of experts from around the world and be a part of the conversation on advancing the practice of coating and paint inspection. Whether you are new to coating and paint inspection or an experienced professional, you'll find valuable resources and a welcoming community in our group.
Updates
-
 pgr380 started the discussion Submerged Coatings DFT Inspection4 months ago
Coating: Modified Polyamine Epoxy
Application: Submerged service; wastewater treatment plant clarifiers
Currently inspecting new submerged coating (Tnemec 66 and 141) for dry film thickness. Specification calls for 4-6 mils primer and 10-15 mils top coat. So total DFT requirement is 14-21 mils. Some of the coating is applied to the inside and outside of a 10 ft diameter drum (open on top and bottom). The remainder is applied to angle iron fabricated into a truss like structure 80 ft long.
There is no spec for testing DFT's other than the implication that any DFT reading cannot be less than 14 mils which is probably unreasonable. However, applying SSPC PA2 (5 avg readings over 100 sq ft) to the drum seems inadequate to me for submerged coatings and since we've had quality control problems with the painter. Any advice on how to tighten up PA2 to catch areas of low DFT's?
Also, PA2 doesn't seem practical when testing small surface areas (such as angle iron). I've proposed taking 4 or 5 readings for each length along each face of each angle (generally 6-8 ft) and averaging that. Any thoughts?
Thanks -
 NDT-Inspect posted an update in the group Coating Inspection3 years ago
Coating inspection is typically performed by visually inspecting the surface to ensure that it meets the specified requirements and standards. This can involve looking for defects such as bubbles, cracks, or other irregularities in the coating. In some cases, more advanced techniques such as infrared imaging or ultrasonic testing may be used to identify problems with the coating that are not visible to the naked eye. Ultimately, the specific methods used for coating inspection will depend on the type of coating, the surface it is being applied to, and the specific requirements and standards that must be met.
A holiday detector is a tool used in the process of coating a surface to detect holidays, or areas where the coating has not been applied properly. This is typically done by applying a high-voltage current to the coated surface and using a specialized instrument to detect areas where the current is not flowing properly, indicating that there is a gap or hole in the coating. Holiday detectors are commonly used in the construction and maintenance of pipelines, tanks, and other industrial structures to ensure that the coating has been applied properly and will provide the necessary protection to the underlying surface.
-
NDT-Inspect posted an update in the group Coating Inspection3 years ago
Coating and paint inspection is a process used to evaluate the condition and performance of coatings and paints applied to surfaces. Coatings and paints are commonly used to protect surfaces from corrosion, wear, and other forms of damage, and to improve their appearance. Coating and paint inspection is performed to ensure that the coatings and paints are applied correctly and are in good condition, and to diagnose any problems that may affect their performance.
Coating and paint inspection typically involves visual inspection, thickness measurement, adhesion testing, and other methods. Visual inspection is used to evaluate the condition and appearance of the coating or paint, including the presence of cracks, bubbles, or other defects. Thickness measurement is used to determine the thickness of the coating or paint, which is an important factor in its performance. Adhesion testing is used to evaluate the bond between the coating or paint and the surface it is applied to, which is critical for its ability to protect the surface.
Coating and paint inspection is typically performed by trained and certified technicians using specialized equipment. The results of the inspection are used to ensure that the coatings and paints are applied correctly and are in good condition, and to identify any problems that may need to be addressed. Coating and paint inspection is an important part of quality control in construction and manufacturing projects, and is essential for ensuring the longevity and performance of the coatings and paints.
-
 4 years ago
What is the best method to perform thickness inspection on diamond wrap? We have a client that has requested thickness testing on a diamond wrap placed on piping with operating temperature of 120 degrees C and diamond wrap thickness = 1.5mm or less. One of the options is use of small diameter, low frequency transducer (like aircraft composite testing) but I am not sure if signal would penetrate thru this type of coating and dead zone could also be present in inspection zone due to small thickness of 1.5mm. Any suggestions or if anybody has had experience with this type of inspection?
👍1 -
NDT-Inspect posted an update in the group Coating Inspection4 years ago
Common Coating Inspection Practices, Standards & Equipment Presentation
👍1 -
NDT-Inspect posted an update in the group Coating Inspection4 years ago
Industrial Coating QA/QC Manual Sample
-
NDT-Inspect posted an update in the group Coating Inspection4 years agoAbout the Coating Inspector Program
For over 30 years, the NACE and SSPC coating inspection certifications have set the global standard for inspectors in the protective coatings industry. Organizations recognize and specify the NACE Coating Inspector Certification Program (CIP) and SSPC Protective Coatings Inspector (PCI) programs due to its comprehensive, hands-on practical testing methods which validate an individual’s knowledge, skills, and experience and elevate the skills of those in the industry.
Who is the Coating Inspector Program for? This program is designed for anyone pursuing a career in coatings inspection or that want to have a greater knowledge of protective coatings for any number of assets (pipelines, storage tanks, key infrastructure, and more).
The curriculum is comprehensive and combines classroom study, discussion, and hands-on practice, the program provides a solid coatings foundation that strengthens the industry’s inspectors and their practices. This program is designed for: Coatings Inspectors Coatings Applicators and Blasters Specifiers, Owner’s representatives, and Technical salesmen
-
NDT-Inspect posted an update in the group Coating Inspection4 years ago
“Do it once, do it right”; carry out a coating inspection
Problems can arise during the pre-treatment, application, and curing phases of a coating job. Coating jobs that at first seem perfect can begin to fail. There are so many variables in any coating application, from the environment to the material itself, that getting an effective long-lasting job is a highly skilled task. This is why we need the coating inspection: we need trained and certified professionals on board at every step, testing and guiding the coating process, as well as making sure the coating job is maintained. Do it once, do it right; the cost of repairing a badly executed coating can be many times the cost to paint it in the first place.
First things first: the coating survey and specification
A coating inspection is carried out by a certified coating inspector who is familiar with all the aspects that contribute to optimal performance of a coating, and the specific standards each coating should individually meet. The coating inspection process starts with inspecting the substrate and the environment, which becomes part of a coating specification. A coating specification is an important document: it should provide clear and precise instructions to the contractor on what is to be done and how it is to be done in order to ensure optimal performance.
The coating survey
First of all you have a facility, infrastructure, asset or machinery that requires coating, or a coating job that needs refurbishing or evaluating. You want assurance that the job will, at every step, be of only the highest quality. Therefore, your coating inspection procedure starts with a site condition survey, which forms a foundation for the coating specification. This condition survey will answer questions such as:
What is the substrate, and its condition (damage, deterioration, rust, peeling)?
To what degree is there damage, what measures must be taken to repair it?
Are there any environmental issues which need to be taken into account?
Any problems that might be found, or maintenance required, need to be dealt with.
Writing the specification
Is your coating specification clear and comprehensive, making sure there are no misunderstandings between engineers, applicators, contractors, and managers? The specification needs to clearly describe the owner’s expectations for their project, aesthetically and structurally. It must also include a description of the substrate and the environment the coating will be applied in. A well-written specification contains as much detail as is required to make these expectations clear, in plain unambiguous terms. It is a template, and thus needs to be as accurate as possible for the finished product to turn out as planned.
Some manufacturers actually provide specification services, so that every step of the process is overseen by someone who knows the coating products inside out.
6 steps of a standard coating inspection from beginning to end
Once the specification has been written, the application process must be monitored from beginning to end; from surface preparation to final colour and gloss. This process generally consists of six standard steps:
coating inspection film thickness gauge
Measuring dry film thickness with an electronic gauge
Inspecting the surface preparation and pre-treatment
The most fundamental phase of a coating inspection. A well-prepared surface is the foundation of a successful coating. The aspects to inspect include surface cleanness and roughness. There are coating inspectors who specialise in assessing surface preparation such as sand blasting.
Assessing climate conditions
Environmental factors such as climate must be assessed to prevent the air, surface temperature, or humidity affecting the curing and adhesion of the coating. The specification should define the optimal application conditions.
Measuring film thickness (before and after curing)
It is important to inspect the film thickness of powder coatings and liquid coatings before the coating cures so that and deviation from the specification can be detected and repaired before curing. The dry film thickness is measured to make absolutely sure the film thickness is in accordance the optimal performance of the coating.
Observing the curing rate
The coating must be cured to the degree defined in the specification; if the coating is not cured enough the surface lacks hardness, making the finished coating layer more vulnerable to hazards such as abrasion and chemicals.
Checking for sufficient adhesion
The current methods of testing adhesion are all destructive, so the test is usually conducted on a sample substrate. It is crucial that the sample has undergone the exact same treatments under the exact same conditions as the real substrate.
Evaluating the colour and gloss of the cured film
The colour of a coating needs to match the specification, but also be consistent across the whole surface. Gloss level is also measured, and checked for deviation.
Prevent damage and analyse failure with regular coating inspections
Even though the coating is in place, the need for coating inspections has not disappeared. Maintenance inspections are conducted to confirm that the coating continues to meet the expectations set in the specification. An examination of all coatings needs to be carried out, to check that properties such as thickness, corrosion, and fire damage all conform to the specification. In offshore and other difficult-to-access environments, the coating inspectors use drones to carry out the inspection. Corrosion costs UK companies billions of pounds a year in replacing and repairing damaged assets, so having a regular coating inspection can catch the problem before it goes too far.
Another form of coating inspection that takes place after the coating has been applied is failure analysis, which is applicable only when the coating does not perform as the specification states. It happens; coating projects fail, damage happens, or corrosion wins. In this case, the coating inspection has one goal – to find the culprit. Like a detective, they will gather and analyse information about the coating, its environment, its usage, its application process and thus uncover the reason behind the failure. Once found, they outline the best way forward to deal with the issue and how to prevent it recurring in the future.
Coating inspection courses and certifications in the UK
There are several coating inspector programmes (CIP) that set the standards for inspection as well as training and certifying inspectors. The most well known and recognised authority is NACE, the Worldwide Corrosion Authority. The NACE certifications and training are given and accepted in the UK. Here you will find information on NACE and other relevant coating inspection programmes for the UK market. Note: ASTM and ISO (International Organisation for Standardization) are the international bodies which produce the standards that guide the coating industry.
NACE Certification
The NACE Coating Inspector Program (CIP) has been setting the standard for inspections in the protective coatings industry for over 30 years. The CIP is an international certification programme that produces the highest calibre of paint inspectors. These come in Level 1, 2, and 3, with 3 being the highest. NACE also publishes a book outlining the use of coating inspection equipment.
CIP Level 1 – This certification is designed for Coating Inspectors responsible for performing and documenting basic and non-destructive inspections of liquid coatings applied by brush, roller or spray to steel surfaces.
CIP Level 2 – This certification is designed for Level 2 Coating Inspectors responsible for performing and documenting non-destructive inspections of liquid and non-liquid coatings to any substrate in a shop setting or under the supervision of a level 3 inspector when working in a field setting.
CIP Level 3 Peer Review – This certification is designed for level 3 coating inspectors (which requires completion of certain requirements, an exam, and approved application) who aim to be recognized as leaders in the Coatings Inspection field.
ICorr Certification
SSPC is the Society for Protective Coatings, and they run training and certification programs and bridging courses for coating inspectors. The PCI is the Protective Coatings Inspector program, and like the NACE certification there are 3 levels, with level 3 being the highest qualification.
ICorr, the Institute of Corrosion, is the British corrosion authority which provides a number of courses that enable paint inspectors to acquire the necessary qualifications to carry out inspections in the field. The courses are in Levels 1, 2, and 3, and are internationally accredited and recognised. The highest level is level 3, and only they are trained and certified to write paint specifications for coatings projects. The ICorr levels correspond to the NACE levels.
SSPC PCI Certification
SSPC PCI Certification -
 5 years ago
Interesting presentation about coating inspection.
-
chack started the discussion What is a NACE Level 1 Coating Inspector? in the group Coating Inspection5 years ago
You will be responsible for performing and documenting basic and non-destructive inspections of liquid coatings applied by brush, roller or spray to steel surfaces under the supervision of a level 2 or 3 inspector when working in a shop setting or a level 3 inspector when working in a field setting.